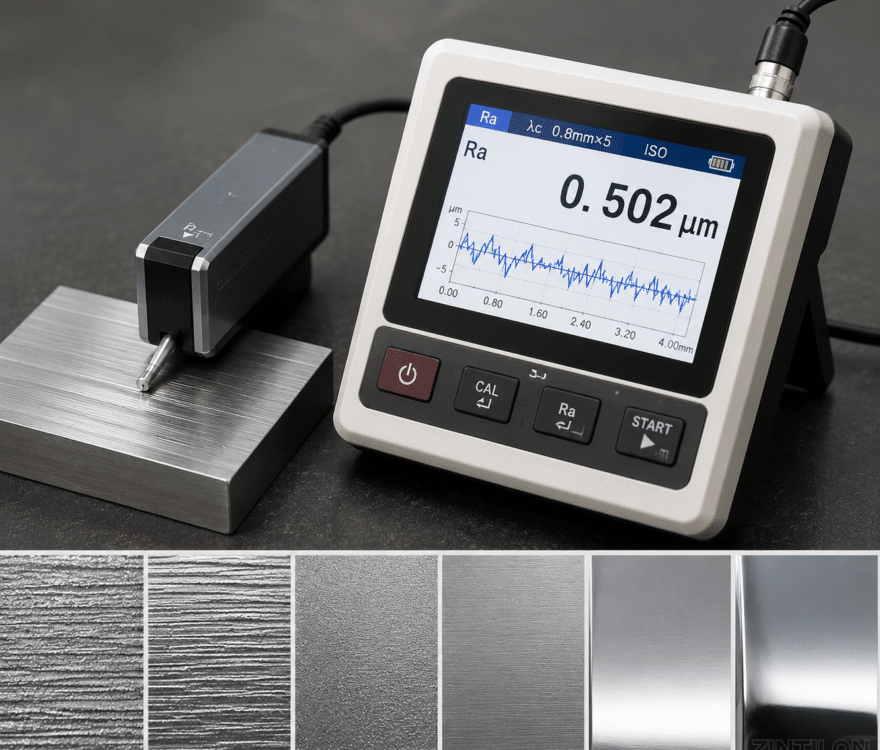
Surface roughness is not just a cosmetic note on a drawing. On a sealing face, it can affect leakage risk. On a sliding surface, it can influence friction and wear. On an anodized aluminum cover, it can change the final appearance. On a non-critical internal pocket, however, a tight roughness requirement may only add machining time and inspection cost.
That is why surface roughness should be specified by surface function, not copied across every face by default.
The sections below focus on how roughness is specified, measured, and reviewed for machined parts.
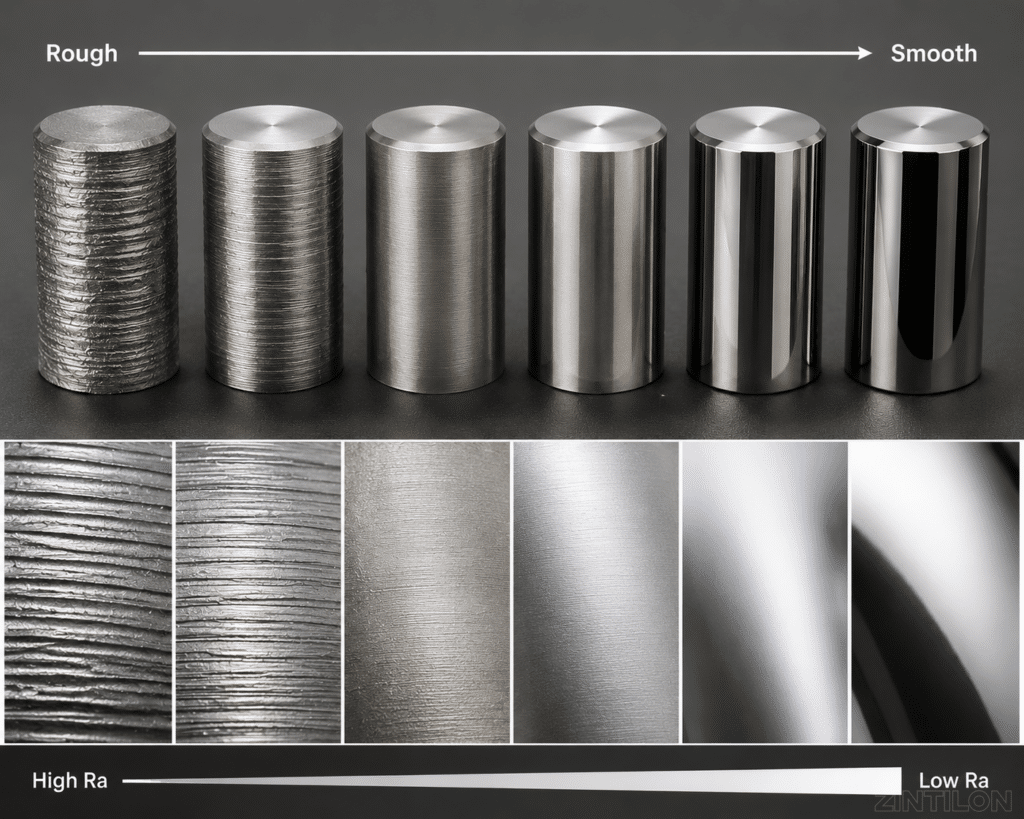
What Is Surface Roughness in Machined Parts?
Surface roughness describes the small peaks, valleys, and irregularities on a manufactured surface. In CNC machining, these features can come from cutting marks, feed patterns, toolpath strategy, vibration, material behavior, tool wear, or post-processing.
A machined surface may look smooth but still have measurable profile variation. That variation can affect sealing, sliding, coating, wear, appearance, and assembly contact.
Surface roughness matters most when the surface has a job to do. A sealing face, sliding bore, bearing contact area, cosmetic cover, and internal relief pocket usually do not need the same finish requirement. The right value depends on what the surface must do.
A lower Ra value is not automatically a better engineering decision. A useful roughness requirement supports the part function without adding unnecessary machining or inspection work.
Surface Roughness vs. Surface Finish vs. Surface Texture
Surface roughness, surface finish, and surface texture are related, but they are not interchangeable.
| Term | What It Means | Manufacturing Relevance |
|---|---|---|
| Surface roughness | Fine peaks and valleys on a surface | Usually measured by Ra, Rz, or related parameters |
| Surface finish | The final surface condition or appearance | May include machining marks, polishing, blasting, anodizing, coating, or other finishing |
| Surface texture | Broader surface geometry | Can include roughness, waviness, lay, and directional pattern |
This distinction matters in drawings and RFQs. “Smooth finish” may work as a general visual preference, but it is not enough for a sealing face, sliding surface, or inspection-controlled feature.
A clearer requirement identifies the parameter, value, unit, and target surface. For example:
Ra 1.6 µm max on the indicated sealing face
This gives the manufacturer and inspector a measurable requirement. “Smooth surface” does not.
When Surface Roughness Affects Part Function
Surface roughness matters when the surface has to seal, slide, accept a coating, meet an appearance requirement, or pass inspection.
A sealing surface may need controlled peaks and valleys to reduce leakage risk. A sliding surface must work with the mating material, lubrication condition, load, and motion. A cosmetic aluminum cover may need a consistent pre-finish surface before anodizing. A coated or painted part may show machining marks if the pre-treatment is not considered early.
| Application | Why Surface Roughness Matters | Common Mistake |
|---|---|---|
| Sealing face | Affects contact and leakage risk | Using “smooth” instead of a measurable callout |
| Sliding surface | Affects friction, lubrication, and wear | Assuming lower Ra is always better |
| Cosmetic surface | Affects visual consistency | Defining only Ra without finish method or visual standard |
| Coated or anodized part | Affects final appearance | Treating machined finish and final finish as the same |
| Assembly interface | Affects seating and contact | Applying tight roughness to every surface |
Surface roughness should be assigned based on risk. A critical sealing face may justify tighter control. A non-functional internal cavity usually does not.
Common Surface Roughness Parameters: Ra, Rz, Rq, and Rt
Ra Surface Finish
Ra, or roughness average, is one of the most common surface roughness parameters on engineering drawings. It describes the average deviation of a surface profile from a mean line.
Ra is useful because it is simple to specify and compare. Its limitation is that it does not fully describe the shape of the surface profile. Two surfaces can have the same Ra value but different peak and valley patterns.
That difference matters on functional surfaces. A surface with occasional deep valleys may behave differently from a more uniform surface, even when both surfaces have similar Ra values.
Rz Surface Roughness
Rz gives more information about peak-to-valley behavior. It may be useful when local peaks, valleys, sealing contact, or wear behavior matters.
Rz is not automatically better than Ra. It measures a different aspect of the surface profile. For many general machined surfaces, Ra may be enough. For sealing, sliding, wear, or fatigue-sensitive surfaces, Rz or another parameter may need review.
Other Roughness Parameters
Rq and Rt may appear in more detailed surface texture requirements. Most general machining discussions focus on Ra and Rz, but Ra is not the only possible control.
| Parameter | What It Describes | Practical Use |
|---|---|---|
| Ra | Average roughness | Common general-purpose roughness callout |
| Rz | Peak-to-valley profile behavior | Useful when deeper valleys or higher peaks matter |
| Rq | Root mean square roughness | More sensitive to larger deviations than Ra |
| Rt | Total profile height | Useful when extreme profile height matters |
For non-critical surfaces, a basic Ra requirement may be sufficient. For critical contact, sealing, sliding, or fatigue-sensitive areas, the roughness parameter should match the surface function.
Surface Roughness Units and General Ra Reference
Surface roughness is commonly specified in micrometers or microinches.
| Unit | Meaning |
|---|---|
| µm | Micrometers |
| µin | Microinches |
| 1 µm | 39.37 µin |
The table below is a general Ra reference. It should not be used as a guaranteed machining capability chart. The actual finish can change with feature access, machining strategy, pre-finish condition, finishing process, and inspection setup.
| Ra µm | Ra µin | General Surface Description |
|---|---|---|
| 0.2 | 8 | Very fine surface |
| 0.4 | 16 | Fine machined or ground surface |
| 0.8 | 32 | Fine machined surface |
| 1.6 | 63 | Common machined surface |
| 3.2 | 125 | Rougher machined surface |
| 6.3 | 250 | Rough surface |
A drawing should show where the roughness value applies. Applying the same tight requirement to every face can increase machining time, finishing cost, and inspection effort.
Surface Roughness Chart by Machining and Finishing Process
Different processes create different surface textures, but the process name alone does not guarantee a fixed Ra or Rz value.
An open milled face, deep pocket wall, small bore, thin-wall feature, and curved surface may all require different machining strategies. The same Ra target may be reasonable on one feature and difficult on another.
| Process | General Surface Tendency | Manufacturing Notes |
|---|---|---|
| CNC milling | Medium to fine | Step-over, cutter condition, toolpath, and setup stability strongly affect the result |
| CNC turning | Medium to fine | Often consistent on round parts, but feed marks may remain |
| Grinding | Fine | May be used when tighter roughness and dimensional control are required |
| Polishing | Fine to very fine | Can improve appearance but may affect edges, flatness, or dimensions |
| Bead blasting | Matte and uniform-looking | Useful for visual consistency, but not a precision roughness-control process by itself |
| Anodizing | Depends on pre-treatment and coating process | Machining marks and surface variation may affect final appearance |
| EDM | Controlled textured surface | Depends on discharge settings and finishing passes |
Use a surface roughness chart for process comparison, not as a promise of final capability. Before choosing a process, review the target surface, feature accessibility, tolerance stack-up, and whether post-processing is allowed.
For parts where surface finish affects function or appearance, the machining plan and finishing plan should be reviewed together. Zintilon supports CNC machining services for projects that require early review of surface requirements.
How Surface Roughness Is Measured
Measuring Surface Roughness with a Surface Roughness Tester
A surface roughness tester is commonly used to measure machined surfaces. A contact-type tester uses a stylus to trace the surface profile and calculate values such as Ra or Rz.
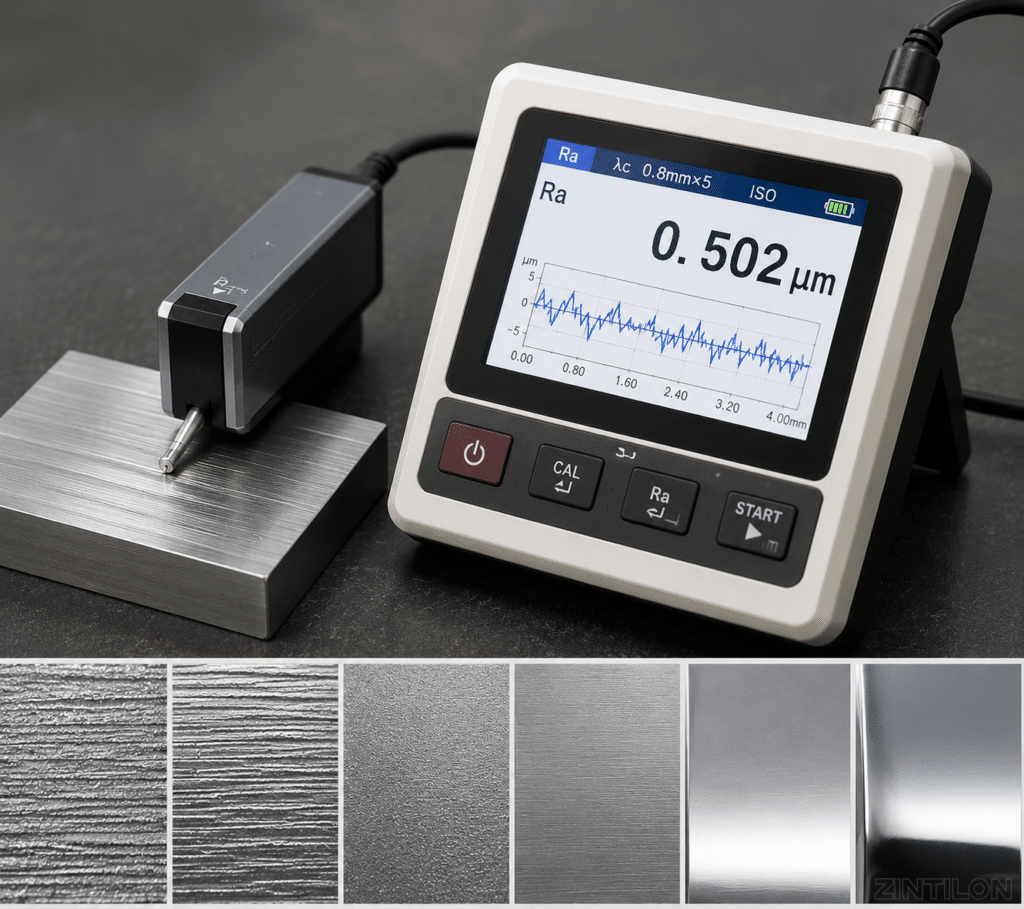
The result can change based on measurement conditions, including:
- Measurement direction
- Measurement position
- Cutoff length
- Evaluation length
- Filtering settings
- Surface cleanliness
- Calibration
- Operator setup
- Directional machining marks or lay
Measurement direction is especially important. Measuring across tool marks may produce a different result from measuring along the toolpath direction. If roughness is critical, the drawing or inspection plan should define where and how the measurement is taken.
Contact vs. Non-Contact Measurement
Contact measurement is common for many machined parts. Non-contact optical methods may be used when a stylus is not suitable, such as on delicate, small, or complex surfaces. Optical measurement can also be affected by reflectivity, surface condition, and equipment settings.
| Measurement Method | How It Works | Typical Use |
|---|---|---|
| Contact stylus tester | A stylus traces the surface profile | Common machined surfaces |
| Optical measurement | Uses non-contact scanning or imaging | Delicate, small, or complex surfaces when suitable |
| Visual inspection | Checks appearance, not precise roughness | Cosmetic screening only |
Visual inspection should not replace measurement when a drawing specifies Ra, Rz, or another controlled roughness parameter.
How to Specify Surface Roughness on Engineering Drawings
A good roughness specification helps the manufacturer choose the right process and helps the inspector verify the result.
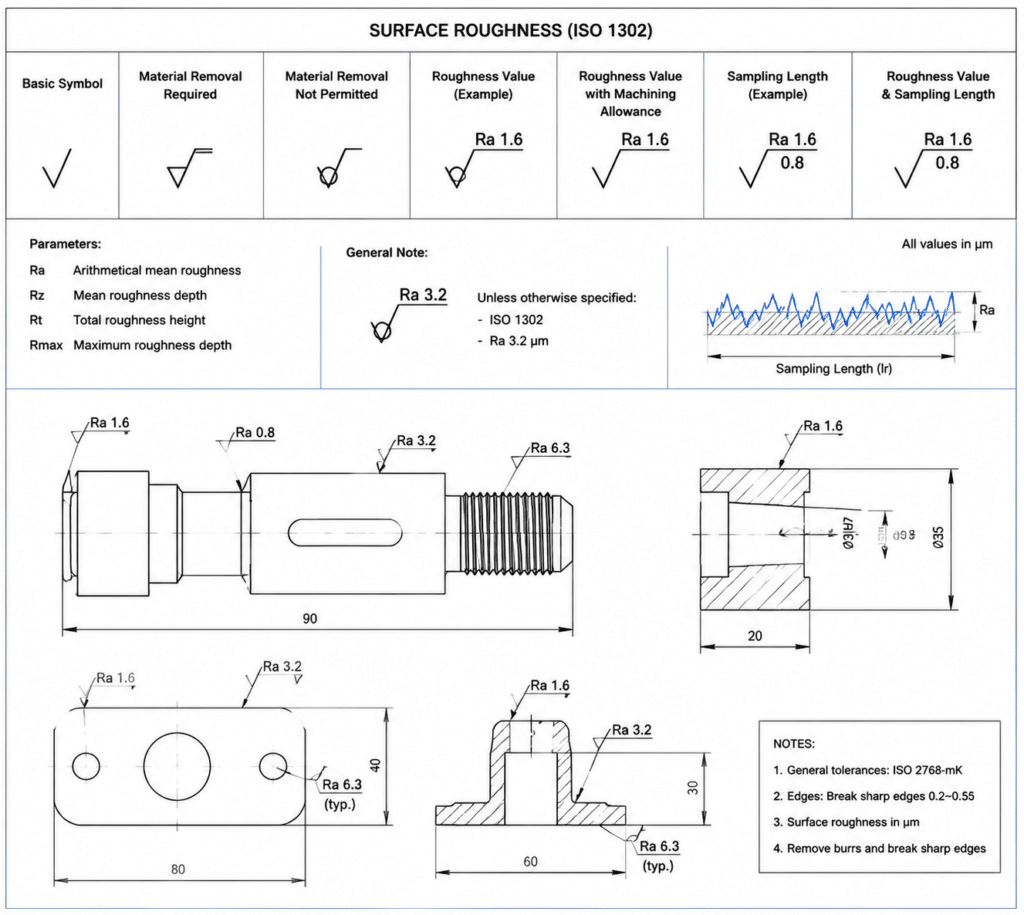
A clear callout should include:
- Roughness parameter, such as Ra or Rz
- Required value and unit
- Exact surface or feature
- Whether post-processing is allowed
- Whether the requirement is functional or cosmetic
- Any special inspection condition, if needed
Avoid vague wording when the surface affects performance.
| Poor Requirement | Why It Is Unclear | Better Requirement |
|---|---|---|
| Smooth surface | Not measurable | Ra 1.6 µm max on indicated sealing face |
| Good finish | Subjective | Define finish process, visual standard, and target surface |
| Polish all surfaces | May add unnecessary cost | Polish only marked cosmetic surfaces; protect critical dimensions |
| Fine machining finish | Too vague for inspection | Specify Ra/Rz value, unit, and target surface |
For cosmetic surfaces, Ra may not be enough. The designer may also need to define the finishing method, texture direction, acceptable tool marks, color expectation, or visual sample requirement.
For functional surfaces, the drawing should identify the target surface and specify the parameter that supports the function.
What to Provide When Requesting a Quote
A roughness requirement is easier to evaluate when the RFQ includes enough technical context.
| Information | Why It Helps |
|---|---|
| 2D drawing | Shows roughness callouts, tolerances, and inspection requirements |
| 3D model | Helps evaluate geometry, access, and machining strategy |
| Material | Affects machinability, tool marks, finishing, and final surface behavior |
| Target surface | Prevents unnecessary control on non-critical areas |
| Ra, Rz, or other parameter | Defines how the surface should be evaluated |
| Unit and value | Reduces ambiguity between metric and imperial requirements |
| Surface finishing requirement | Clarifies polishing, blasting, anodizing, coating, or other treatments |
| Functional or cosmetic purpose | Helps select the process and inspection approach |
| Inspection requirement | Aligns measurement method and reporting expectations |
With this information, the supplier can price the right surfaces instead of assuming the tightest finish applies everywhere.
Choosing the Right Surface Roughness for Machined Parts
The right roughness value depends on what the surface does.
Before specifying Ra or Rz, ask:
- Does the surface seal, slide, support load, locate another part, or affect appearance?
- Is the surface functional, cosmetic, or non-critical?
- Is CNC machining enough, or is finishing required?
- Will coating, anodizing, polishing, or blasting be applied after machining?
- Could the roughness requirement affect tolerance, edge condition, or flatness?
- Does the surface need inspection documentation?
| Surface Type | Roughness Decision | Cost or Quality Consideration |
|---|---|---|
| Sealing surface | May need controlled Ra and possibly Rz | Poor control can increase leakage risk |
| Sliding surface | Consider friction, lubrication, and wear | Too rough or too smooth may both cause issues depending on the design |
| Cosmetic exterior | Focus on consistent appearance | Finish method and visual standard may matter more than low Ra alone |
| Internal non-critical surface | Standard machined finish may be enough | Over-specification adds cost without function |
| Coated or anodized surface | Consider pre-finish and final finish together | Machining marks may show through the final treatment |
| Prototype surface | Match the test purpose | Avoid production-level finish unless needed for testing |
Tighter roughness should be used where it reduces functional or appearance risk. It should not be copied across the whole drawing without reviewing each surface.
How Surface Roughness Affects Cost, Lead Time, and Quality
A lower Ra value usually requires more process control. Depending on the part, it may require slower cutting, toolpath refinement, secondary finishing, or additional inspection.
Tighter roughness requirements can affect:
- Machining time
- Tool wear
- Setup control
- Finishing cost
- Inspection workload
- Rework risk
- Production planning
Under-specifying roughness can create quality problems. A sealing face may leak. A sliding surface may wear too quickly. A cosmetic surface may show tool marks after anodizing. A coated part may have inconsistent appearance.
Over-specifying roughness creates a different risk. A non-critical surface may become more expensive to machine and inspect without improving part performance.
The best specification is not the smoothest surface. It is the surface condition that supports the function with the least unnecessary manufacturing complexity.
Practical Application Scenarios
Sealing Surface on a CNC Machined Housing
A machined housing may include a sealing face where roughness affects contact and leakage risk. A note such as “smooth surface” is not precise enough for this feature.
A better approach is to identify the sealing face on the drawing and specify the roughness parameter, value, and unit. If peak-to-valley behavior matters, the engineer may need to consider Rz or additional inspection requirements instead of relying only on Ra.
Cosmetic Aluminum Cover with Anodizing
For a visible aluminum cover, the final appearance depends on more than machining. Tool marks, polishing direction, blasting texture, pre-treatment, and anodizing can all affect the final look.
The designer should identify which surfaces are cosmetic, whether visible machining marks are acceptable, and what finishing process is expected. If appearance consistency is critical, a visual sample or finish standard may be more useful than a roughness value alone.
Sliding or Contact Surface
For a sliding surface, a lower Ra is not automatically the best choice. The surface must work with the mating material, lubrication condition, load, and expected wear behavior.
The drawing should identify the functional surface and specify the required roughness parameter. The manufacturing team may also need to review material, geometry, and machining access before confirming the process route.
How Zintilon Supports CNC Machining and Surface Finishing Requirements
Surface roughness requirements are easier to manage before production than after machining has started.
For machined parts with specific surface finish requirements, Zintilon can review drawings, materials, tolerances, critical surfaces, and finishing expectations to help evaluate a practical manufacturing approach.
This review may include CNC machining strategy, surface finishing considerations, and communication around which surfaces require tighter control. For prototypes, small-batch production, or parts with functional surface requirements, early review can reduce uncertainty in quoting, production planning, and inspection.
Learn more about Zintilon’s CNC machining services or share your project details through the request a quote page.
FAQs About Surface Roughness
Is surface roughness the same as surface finish?
No. Surface roughness is a measurable part of the surface condition. Surface finish is broader and may include machining marks, appearance, polishing, blasting, anodizing, coating, or other post-processing results.
What does Ra mean in surface roughness?
Ra means roughness average. It describes the average deviation of a surface profile from a mean line. Ra is common because it is easy to specify and compare, but it does not describe every peak and valley on a surface.
What is the difference between Ra and Rz?
Ra describes average roughness. Rz gives more information about peak-to-valley behavior. Ra may be enough for many general surfaces, while Rz may be useful for sealing, sliding, wear, or other functional surfaces where local peaks and valleys matter.
How do you measure surface roughness?
Surface roughness is commonly measured with a contact surface roughness tester or a non-contact optical method. Measurement direction, cutoff length, evaluation length, calibration, filtering, and surface condition can affect the result.
Is a lower Ra always better?
No. A lower Ra can increase machining time, finishing cost, inspection requirements, and lead time. The right roughness value should match the part function and finishing method.
What should be included in an RFQ for surface roughness requirements?
Include the drawing, target surfaces, Ra or Rz value, unit, material, surface finishing requirement, and any inspection expectations. This helps the supplier review the correct surfaces instead of treating the whole part as a tight-finish requirement.
Need Surface Roughness Review for a Machined Part?
For machined parts with defined surface roughness or finishing requirements, send Zintilon your drawing, material, tolerance, and surface finish notes for a manufacturing review before production.
Great, Together


